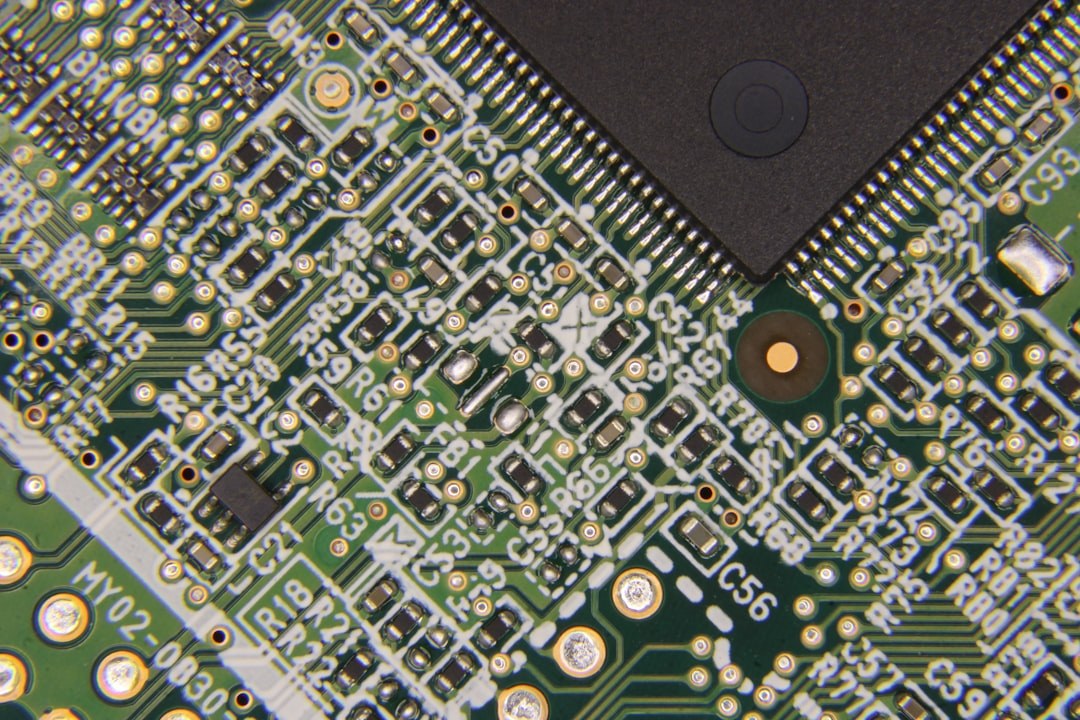
As component densities on printed circuit boards continue to rise and manual inspection becomes statistically unreliable at production volumes, Automated Optical Inspection — universally abbreviated AOI — has evolved from an optional add-on into a mandatory process step in virtually every professional SMT assembly environment. AOI systems capture and evaluate visual information about a populated PCB in order to detect assembly defects such as missing components, misalignment, tombstoning, solder bridges, insufficient solder and polarity reversals. Unlike functional test methods, AOI operates non-destructively and at inline production speeds, making it suitable for 100-percent inspection coverage without throughput penalty.
Despite the apparent simplicity of the concept — a camera looks at a board and compares what it sees against a reference — the practical implementation of AOI involves a sophisticated interplay of illumination physics, imaging optics, sensor technology, image-processing algorithms and statistical process control. A thorough understanding of these layers allows process engineers to select the right system architecture, configure inspection programs effectively and interpret AOI results in a way that genuinely drives yield improvement rather than generating noise.
Illumination and Imaging: The Physical Foundation
The optical quality of the captured image is the single most critical hardware parameter in an AOI system, because downstream algorithms can only work with the information that the sensor actually receives. Most modern AOI systems use structured, multi-angle LED illumination arranged in concentric rings or dome configurations around the optical axis. By combining light sources at different elevation angles — typically high-angle, mid-angle and low-angle — and in different colours, the system encodes three-dimensional surface information into a two-dimensional image through photometric stereo techniques. A solder joint that appears flat and featureless under diffuse top-down light will reveal its characteristic concave meniscus shape when illuminated from a shallow angle, allowing the algorithm to distinguish a good fillet from a cold or insufficient joint.
Camera resolution is typically specified in micrometres per pixel. For standard SMT components down to 0402 metric (imperial 01005) package sizes, resolutions in the range of 10 to 15 µm per pixel are commonly used. Ultra-fine-pitch BGA inspection or chip-scale packages may require dedicated optics with sub-10 µm resolution. The trade-off between field of view and resolution determines how many camera positions — and therefore how much time — are required to cover a full board panel, directly affecting throughput.
2D versus 3D AOI: Architecture Comparison
First-generation AOI systems operated exclusively in two dimensions, analysing colour, contrast and geometric shape from a single top-down perspective. While 2D AOI remains cost-effective for less complex assemblies, it has inherent limitations: it cannot reliably distinguish between a correctly placed component at the right height and a component that is slightly lifted on one side (head-in-pillow defect), nor can it measure solder paste volume after reflow independently of component shadow effects.
Three-dimensional AOI systems address these limitations by reconstructing the actual topography of the board surface. The dominant method is phase-shift profilometry, in which a structured light pattern — typically sinusoidal fringe patterns projected by a DMD or LCD projector — is projected onto the board at multiple phase offsets. The camera captures the distorted fringe pattern, and dedicated algorithms compute a height map with sub-micrometre repeatability. This height map allows the system to measure component stand-off height, solder joint volume and coplanarity, parameters that are invisible to purely 2D imaging. The practical consequence is a significantly lower false-call rate and improved detection of defect categories that previously escaped 2D inspection.
Inspection Program Development and the False-Call Dilemma
The effectiveness of an AOI system in production is determined far more by the quality of its inspection programs than by the raw capability of the hardware. An inspection program defines, for each component on the board, the region of interest, the expected reference image or geometric model, and the tolerance windows within which a result is classified as „pass'. Tolerance windows that are set too tightly generate false calls — escapes classified as defects — which consume operator time for unnecessary re-inspection and erode confidence in the system. Tolerance windows set too loosely allow genuine defects to pass undetected.
This trade-off is quantified through two metrics borrowed from statistical process control: the false-call rate (FCR), expressing how often a good board or component is incorrectly flagged, and the defect escape rate (DER), expressing how often a genuine defect passes the inspection gate. Modern AOI platforms assist program development through statistical learning features that analyse a batch of known-good boards to automatically propose tolerance limits that minimise both metrics simultaneously. Nevertheless, initial program generation, golden-board teaching and ongoing maintenance as product revisions occur remain significant engineering investments that are frequently underestimated during system procurement.
Placement within the SMT Process Flow
AOI stations can be positioned at multiple points in an SMT line, and the strategic placement determines which defect categories can be caught and at what cost. Pre-reflow AOI, placed after the pick-and-place machine and before the reflow oven, detects placement errors — missing components, wrong polarity, misalignment — while the board is still in a state where rework is cheap: a misplaced component can simply be repositioned without soldering rework. Post-reflow AOI, the most common single AOI position, inspects the final soldered assembly and catches the full spectrum of soldering defects in addition to any placement errors that survived reflow.
A dual-AOI strategy — one system pre-reflow and one post-reflow — maximises defect localisation and minimises rework cost per defect caught. The pre-reflow system filters out placement defects early, reducing the population of defective boards entering the oven and providing immediate feedback to the pick-and-place process. The post-reflow system then focuses exclusively on soldering quality, with inspection programs optimised accordingly. This separation also enables statistical process control feedback loops to individual upstream process steps, which is a prerequisite for genuinely closed-loop smart-factory operation.
Integration with MES and Closed-Loop Process Control
A stand-alone AOI system that produces a pass/fail verdict for each board is operationally useful but leaves significant value on the table. The real power of AOI emerges when inspection data are fed into a Manufacturing Execution System (MES) or a dedicated process analytics platform, where defect patterns can be correlated with upstream process parameters. If the AOI system consistently flags solder bridging on a specific fine-pitch connector package, and that pattern correlates with a particular stencil printing time-of-day or squeegee pressure setting, the root cause can be identified and eliminated rather than simply reworked board by board.
Modern AOI systems export structured defect data via standardised interfaces — most commonly following the IPC-CFX (Connected Factory Exchange) protocol or proprietary XML/JSON formats — that MES platforms can ingest in real time. Component-level traceability, in which the AOI result is linked to the serial number of each component via 2D barcode or RFID scanning, further enables retrospective analysis across production lots and supports field-return root-cause investigations. This connectivity layer transforms AOI from a quality gate into an active node in a data-driven manufacturing intelligence architecture, a transition that defines the direction of the discipline for the foreseeable future.
Practical Considerations for System Selection and Operation
When specifying an AOI system, engineers should evaluate not only measurement performance metrics such as resolution, repeatability and throughput, but also the ergonomics of the programming environment, the availability of component libraries, the robustness of the conveyor and handling mechanism to the board sizes and weights in use, and the openness of the data export interfaces. Vendor support for IPC standards — particularly IPC-7711/7721 for rework and IPC-A-610 for acceptability criteria encoded into the inspection logic — is a practical indicator of how well the system will integrate into a standards-driven quality management framework.
The ongoing evolution of AOI is being shaped by the adoption of deep-learning-based image classifiers, which supplement or partially replace rule-based algorithms. Neural networks trained on large libraries of defect images can generalise across component variants and board finishes in ways that hand-coded classifiers cannot, reducing both false-call rates and the engineering time required for program maintenance. As these AI-assisted inspection capabilities mature and the cost of 3D imaging hardware continues to decline, AOI systems with true three-dimensional measurement at inline speeds are expected to become the standard configuration across the full spectrum of electronics manufacturing, from high-volume consumer electronics to low-volume, high-mix industrial and medical applications.