
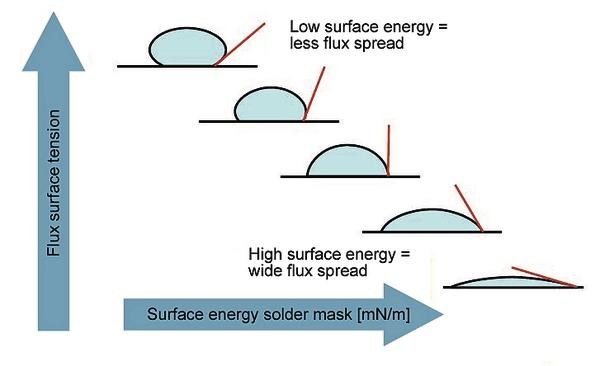
- Spreading. In selective soldering the flux should not spread too far. Flux is only required in the soldering area and should remain there only.
- Inert after soldering. Non-activated flux residues are a potential risk for electro-migration.
- Flux surface tension (flux type)
- Surface energy of the board (solder mask)
- Temperature of the flux
- Temperature of the board
- An alcohol flux will spread less when the board is preheated, where a VOC-Free water based flux will spread more when the surface is hot.
- Due to the minor spreading the solid content left per cm² is much more for a VOC-Free flux and less for alcohol based.
- Open time drop-jet (500 – 2500ms)
- Frequency drop-jet (10 – 300Hz)
- Speed of the flux robot (10 – 150mm/s)
- 1.) “Performing Flux-Technology for Pb-Free SN100C Solders”, Apex 2010, Ineke van Tiggelen-Aarden, and Eli Westerlaken, Cobar Europe BV
- 2. ) “How PEDOT:PSS solutions produce satellite-free inkjets”, Stephen D. Hoath, SungjuneJunga, Wen-Kai Hsiaoa and Ian M. Hutchingsa, Department of Engineering, University of Cambridge

