
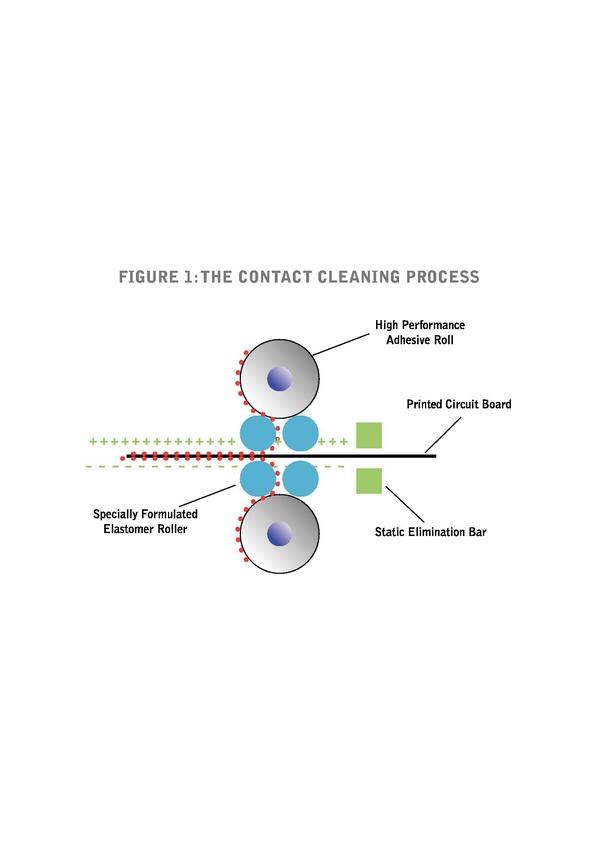
- There are two types of process from a contamination viewpoint: First, those which generate contamination as a fundamental part of the process such as drilling or wet processing. Second, those which are sensitive to contamination like solder paste printing, resist application and exposure.
- Plans should be prepared for every area to be audited showing the layout of all the equipment in the room and the position of all doors.
- Any other points where material or product comes into the production area should be noted.
- A corner of the plan should be reserved for notes to record what type of clothing the operators are wearing and any other relevant information.
- The plans will be used to record exactly where samples are taken so that the exercise can be repeated under controlled conditions.
- A device called a tyndleometer is used to assess air quality in a production environment. Sampling is very rapid so that real-time analysis of the samples can be undertaken. The position of where the samples were taken is marked on the department plan.
- Surface contamination is collected using a special hand-held roller which is passed over the surface to be tested. The particles collected are then transferred on to an adhesive pad with a grid pattern on it. The sample is transferred to a release sheet which has details of the exact location of the sample.
- Sample analysis is carried out using a microscope with a variable magnification of up to 60x to examine each square in the sample grid. The type and number of each type of particle should be recorded in the department contamination matrix.
- If there are any unusual or unidentifiable particles in the sample, colour photographs should be taken for further reference and investigation.
- 1. Human hair – a person loses, on average, 50 hairs per day.
- 2. Lint – although specialist cleaning cloths used in the production area are supposedly “lint free” they can still snag when used for wiping pad areas and stencils, creating loose fibres which can enter the production process.
- 3. Clothing fibres – fibres from operator’s clothing are a frequent source of contamination.
- 4. Dust – the main source of dust is shed human skin. On average a person breathes 700,000 skin flakes per day and discards one layer of skin every day.
- 5. Production plant – particles from ceilings, floors, shelving as well as packaging materials can enter the production line.
- 6. Epoxy dust – during the manufacture of bare boards every effort is made to remove any contaminants. However, after routing only the top surface can be cleaned leaving loose dust on the edges.
- 7. Glass splinters – PCBs can produce loose glass from snap outs or routing.
- 8. Solder paste – loose solder paste can remain on misprinted boards which are wiped “clean” and sent back through the production line.
- 9. Solder resist – this can flake off leading to contamination.
- 10. Packaging materials – boards often come individually wrapped in paper. When removed some paper fragments can cling to the board due to static.
- Contamination in the solder paste can cause craters in the solder during the reflow process.
- Particles can block stencil holes leading to an incomplete print.
- Contamination can cause tombstoning whereby the chip component stands on end with one end not connected.
- Fibres from cloths used to clean stencils can become trapped between pads leading to short-circuits.
- Contamination can also lead to unreliable solder joints and poor solder wetting.

