
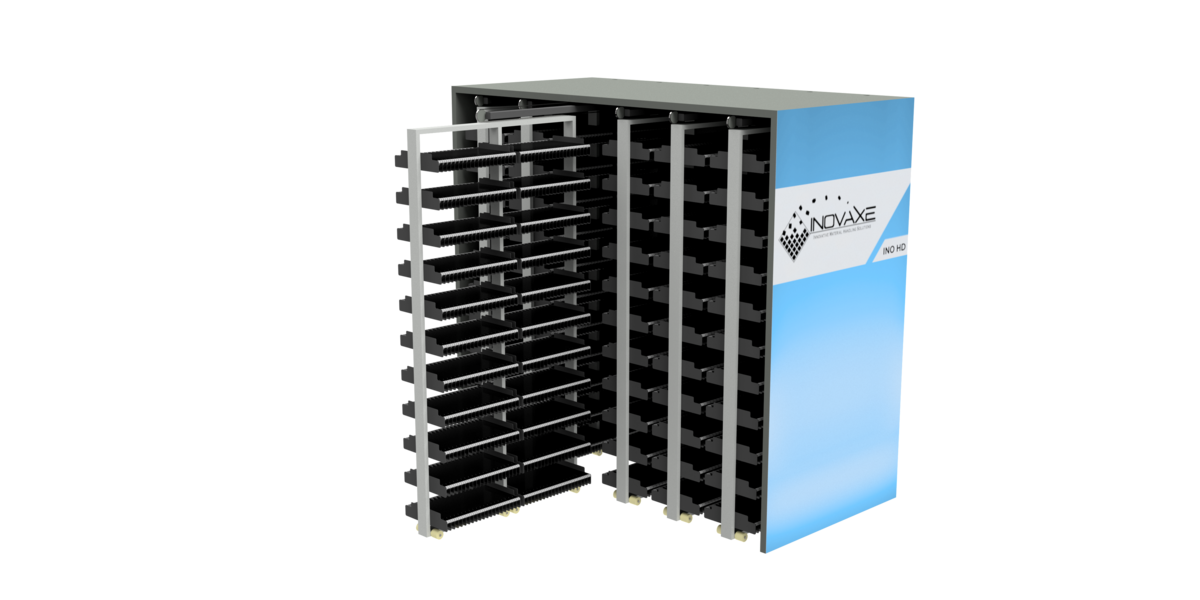
InoHD is designed to address one of the most persistent challenges in electronics manufacturing: space. The system removes the need for traditional storage aisles by combining servo-driven mobile shelving with the company’s smart sensing and pick-to-light technology. This approach allows manufacturers to store up to 310 SMT reels per square foot, while still providing fast, guided access and real-time inventory verification.
Unlike conventional storage towers, the solution enables operators to access materials directly at the point of need, with built-in verification that helps eliminate picking errors. Customers can dramatically reduce storage floor space by fitting over 10,500 SMT reels into an area as compact as 4 ft × 8 ft—far more efficient than traditional stockroom layouts. The system is modular, scalable, and designed to integrate with existing MES and ERP platforms, helping reduce labor time and unnecessary material handling.
“With InoHD, we focused on solving real space and workflow problems—not just packing more reels into a smaller footprint,” said Ben Khoshnood, President and CEO of Inovaxe. “The goal was to give manufacturers better access, better accuracy, and better use of their floor space without adding complexity.”
In addition to InoHD, the company demonstrated its broader portfolio of smart material handling solutions, including mobile Smart Racks, line-side storage systems, and stencil rack solutions. The company was also joined by its MODI partner from Germany, who demonstrated the V5 incoming goods scanner, highlighting automation for receiving and inventory verification.
The live demonstrations held at the company’s booth invited attendees to rethink efficient material flow across the factory floor.



